Yingtai Chemical Co., Ltd.
Yingtai Chemical Co., Ltd.


Ethylene glycol is the simplest diol and a critically important basic chemical raw material. It is primarily used as a monomer for polyester fiber (polyethylene terephthalate fiber, PET fiber) and polyester resins, a key component in automotive antifreeze/coolants, and also in the production of unsaturated polyester resins, surfactants, plasticizers, and explosives (nitroglycol).


Versatile Industrial Raw Material for Fiber and Resin Manufacturing
Ethylene Glycol (MEG) with CAS 107-21-1 serves as a foundational raw material predominantly used by industries producing polyester fibers (PET) and unsaturated polyester resins. This chemical targets industrial manufacturers requiring highly pure glycol to ensure polymerization efficiency and product consistency. As a viscous, colorless liquid with superior hygroscopic qualities, MEG ensures process stability in various chemical syntheses. Our role as reliable specialty chemicals suppliers supports industrial clients demanding stable quality and supply continuity in their value chain integration.
Distinguished Chemical Properties and Purity Metrics
Ethylene Glycol produced here boasts a purity of no less than 99.8%, certified through stringent quality controls facilitating low impurity profiles including minimal diethylene and triethylene glycol content. The manufacturing process employs advanced direct or catalytic hydration of ethylene oxide, yielding a colorless, odorless liquid with a melting point of -12.9°C and boiling point of 197.3°C. Its molecular formula C2H6O2 and full miscibility in water underpin its function as a freezing point depressant and desiccant. Measurement of viscosity at 21.0 mPa·s (20°C) assures compatibility with controlled industrial processes. This product aligns with technically demanding specifications encountered by industrial chemicals manufacturers.
Industrial Applications Spanning Textiles to Automotive Coolants
Our Ethylene Glycol is a vital component across multiple sectors including textile fiber production, plasticizers synthesis, and automotive antifreeze formulations. Its integration into polyethylene terephthalate fiber manufacturing is critical for polymer chain formation, while its role in coolant formulations enhances thermal management in automotive engines. Further uses include gas dehydration and glycol ether solvent production within industrial cleaners formulations. Partnering as a specialty chemicals supplier enables us to address diverse industrial cleaning chemicals suppliers’ demands requiring precise chemical performance for process optimization.
Strategic Manufacturing and Quality Control Infrastructure
Our ethylene glycol benefits from advanced process technologies executed in a state-of-the-art production plant located in Shandong. This setup enables industrial chemicals manufacturers to receive product with consistent purity and minimized impurities. The modular design of our production lines, combined with intelligent control systems, facilitates scalable volumes suitable for both fiber-grade and industrial uses. This technical robustness ensures product batches conform to rigorous purity and performance parameters sought by industrial cleaners and cleaning chemicals suppliers, emphasizing supply reliability and product integrity.
Enhanced Chemical Performance Meets User Operational Requirements
The product’s purity and physicochemical stability deliver tangible performance advantages, including strong hygroscopicity and broad miscibility, critical for formulation stability in industrial cleaners and antifreeze applications. Its compatibility with established process systems supports easy integration and predictable results. Users benefit from minimized downtime due to consistent product quality, while obtaining cost-effective raw material procurement from a trusted specialty chemicals supplier. This alignment of performance and usability fosters dependable process workflows essential for industrial chemicals manufacturers.
|
Ethylene glycol — MEG, monoethylene glycol, or 1,2-ethanediol — is the simplest saturated diol and one of the base chemicals the rest of the industry is built on. We produce it at Dongying in Shandong by hydrating ethylene oxide, and it leaves the plant at ≥99.8% purity with the diethylene glycol (DEG) and triethylene glycol (TEG) homologues held low.
At room temperature it is a colourless, odourless, transparent liquid, clearly more viscous than water and miscible with it in every proportion. That miscibility is what most of its working life depends on: it lets a coolant blender build a single-phase fluid with a controlled freeze point, and it lets a polyester plant feed a liquid monomer stream with no solvent carrier and no dispersion step.
Two markets absorb nearly all of the world's supply. Over half goes into polyester, where it condenses with purified terephthalic acid to make PET — fibre, bottle resin, film and engineering plastics. Roughly a quarter to a third becomes the base fluid of automotive and industrial antifreeze and de-icing fluids. The balance runs into unsaturated polyester resins, glycol ethers, surfactants, plasticizers, gas dehydration and nitroglycol, and it is that smaller stream that resin plants, glycol ether producers and formulators of industrial cleaners buy into.
Most buyers ask the same three questions before they commit: is the purity high enough and steady enough for my reaction, is the water and acidity low enough to leave my catalyst and my corrosion package alone, and can this specialty chemicals supplier hold the same numbers month after month. The sections below give you the figures to answer them.
| Property | Value |
|---|---|
| CAS number | 107-21-1 |
| EINECS number | 203-473-3 |
| Molecular formula | C₂H₆O₂ |
| Purity | ≥99.8% (industrial / fiber grade) |
| Appearance | Colourless, odourless, transparent viscous liquid |
| Melting point | -12.9 °C |
| Boiling point | 197.3 °C |
| Viscosity | 21.0 mPa·s at 20 °C |
| Vapour pressure | 0.01 kPa at 20 °C |
| Water solubility | Miscible with water in all proportions |
| Acidity | Neutral |
| Flash point | 111 °C (closed cup) |
| Origin | Shandong, China |
Blended with water and an inhibitor package, this glycol does three things at once: it depresses the freeze point far below what water alone can reach, it raises the boiling point so a hot engine does not vent its coolant, and through the inhibitors it protects the metals in the loop from corrosion and scale. That combination is why antifreeze is the second-largest outlet for the material, and why a coolant base fluid is specified around water content and acidity as much as around the assay.
Most of the coolant blenders we ship to are industrial chemicals manufacturers who buy MEG as a base fluid and build their own inhibitor and dye package on top of it. They want it clean and additive-free, and they want it to respond predictably when they dilute it: no colour body, no acid, no drift in water content between containers. Water quality in the finished blend is their part of the job; ours is keeping the base fluid's water, acidity and homolog levels exactly where their formulation was designed around them.
The same base fluid goes into de-icing and hold-over fluids for aviation and ground equipment, into coolant for stationary engines and generator sets, and into heat-transfer loops that need a predictable freeze point. Each finished product has its own target, so the practical move for a blender is to send us the freeze point and the inhibitor system they are working to, and confirm the base-fluid specification against it before the first bulk order.
The working specification is ≥99.8%, and the number that sits behind it is the homolog figure. Diethylene glycol and triethylene glycol are the natural by-products of the ethylene oxide hydration route, and in PET they do not stay inert — they enter the polymer chain and shift the melting behaviour and colour of the finished resin. Keeping both low is the difference between a glycol a polymeriser can feed blind and one that has to be trimmed batch by batch. Water matters for a similar reason: it pushes the esterification equilibrium the wrong way and adds to the energy a line has to spend removing it. Neutral acidity means no free acid is carried into a reactor or into a coolant loop, where it would go to work on the metals.
Appearance is the quick check that sits on top of the specification. This grade is colourless, odourless and clear, with no haze and no colour body. Any tint or cloudiness in a sample is worth a conversation before the container is accepted, because in polyester and in coolant alike, colour travels straight through to the finished product.
Consistency is what industrial chemicals manufacturers actually buy. Two lots can both read ≥99.8% and still behave differently if the water or the DEG drifts inside the tolerance, so we control the process rather than test the batch into specification. Set the numbers next to your own incoming specification before you commit to a monthly programme, and tell us which of them are tight for your line — those are the ones we watch hardest on repeat orders.
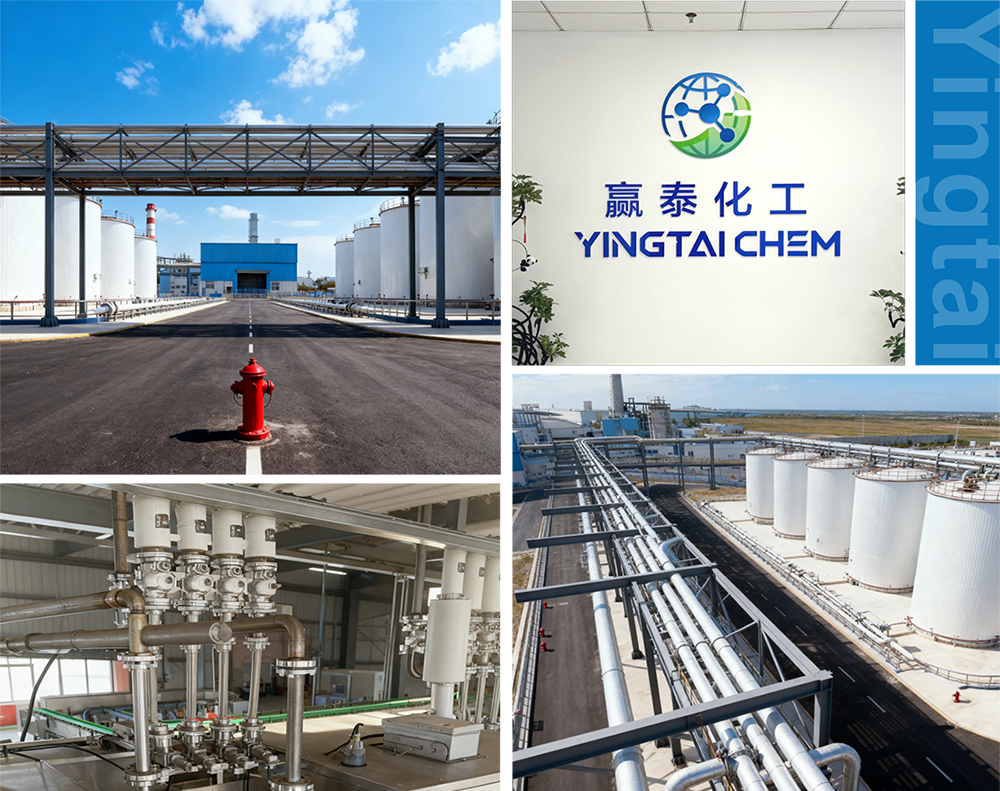
Shandong Yingtai Chemical Co., Ltd. operates from Dongying, Shandong, in the heart of China's petrochemical industry and home to the Shengli Oilfield. Our 60,000㎡ park-based facility runs modern plants with automated control systems and integrated utilities, and a team of over 200 people covers R&D, production and sales of high-value-added fine chemicals. We supply seven core chemical categories, backed by stable quality and consistent availability, and work alongside buyers on sourcing, product application and technical support. Custom requirements are reviewed case by case — share your specification and volume and we will confirm feasibility.
They are close relatives with different jobs. DEG is the dimer that forms alongside MEG in the same hydration route, with a higher boiling point, higher viscosity and noticeably higher toxicity. MEG is the monomer that polyester and antifreeze are built on, and this grade is specified at ≥99.8% with DEG and TEG held low precisely so that what you feed the reactor is MEG rather than a mixture. If your formulation calls for DEG, that is a separate product with its own specification, and the two should not be swapped in a coolant package or a polymerisation recipe.
Not as a cleaning agent in its own right — it is not a detergent and is not formulated into a cleaner as the active ingredient. Its role is upstream: it is the feedstock for the glycol ethers and the surfactant intermediates that cleaning chemicals suppliers build their formulations around. Buyers in that sector usually order the glycol to feed an ether or ethoxylation unit, and they care about water content and consistency far more than about cleaning performance.
It mixes with water in all proportions, so there is no separation point at any ratio. That is what makes it useful in a coolant: the blend's freeze point falls as the glycol share rises, and its boiling point rises at the same time. The exact freeze point you reach depends on the ratio and on the inhibitor package in the finished fluid, so if you are building a coolant to a target figure, send us the target and confirm the base-fluid specification against it rather than assuming one fixed dilution.
Yes — this is the grade the polyester chain is built around. The assay is ≥99.8%, water and acidity are held low, and DEG and TEG stay inside the window a polymeriser can tolerate, because both enter the chain and change the resin's melting and colour behaviour. Industrial chemicals manufacturers running continuous PET lines are usually the first to notice a drift.
Because the hazard is real and slightly unusual. The liquid is toxic if swallowed, and it is sweet enough to be mistaken for a drink — which is how most serious incidents start, with a decanted bottle left on a bench or a container reused for something else. Handled properly, in labelled closed containers with gloves, goggles and a bund, it is a routine industrial liquid. Our handling notes are written for the people who decant and store it, not for the driver who buys a sealed coolant.
We supply one industrial / fiber grade at ≥99.8%, produced at Dongying by ethylene oxide hydration. Grades outside that range — regulated food, pharmaceutical or cosmetic grades, for example — are not what this line is set up for, so it is worth saying early if your process needs one. As a specialty chemicals supplier we will set your specification sheet against our own and tell you plainly where we match it and where we do not, before you plan a trial.